Case Studies
Aerospace-Grade 5-Axis Machining---Built on Self-Developed Gantry Machine Tools
Precision CNC Machining of C919 Wing Panel — 9m Aerospace Structure
Sep. 01, 2026
Share:

Project Background
The C919 is China's first domestically developed large commercial aircraft, with a wingspan of 35.8 meters. Each wing requires a set of precision-machined aluminum structural panels and rib components that form the primary load-bearing wing structure. These panels must maintain dimensional stability across a 9-meter span while meeting the ±0.015mm positional accuracy required for aerospace structural fastening. The project's Tier-1 supplier faced a tight production schedule and needed a machining partner capable of delivering full-scale panels in a single setup — without multi-part assembly and joinery that would introduce cumulative positional errors.
Technical Challenges
The C919 is China's first domestically developed large commercial aircraft, with a wingspan of 35.8 meters. Each wing requires a set of precision-machined aluminum structural panels and rib components that form the primary load-bearing wing structure. These panels must maintain dimensional stability across a 9-meter span while meeting the ±0.015mm positional accuracy required for aerospace structural fastening. The project's Tier-1 supplier faced a tight production schedule and needed a machining partner capable of delivering full-scale panels in a single setup — without multi-part assembly and joinery that would introduce cumulative positional errors.
Large-Scale Single-Setup Machining
Machining a 9.2-meter aluminum panel to aerospace tolerances in a single setup required a gantry-type 5-axis machining center with a travel envelope far beyond standard CNC shops.
Thin-Wall Structural Integrity
The panel design featured thin-web ribs as narrow as 2.5mm between machining features, creating severe chatter and deflection risks during cutting. Conventional clamping methods would distort the part under machining loads.
300+ Machined Features
Over 300 fastener holes, lightening pockets, and structural bosses needed to be machined to ±0.015mm positional accuracy — with full CMM documentation per AS9102.
Aerospace-Grade Surface Integrity
No burrs, micro-cracks, or heat-affected zones permitted. Surface finish at rib walls needed to meet Ra ≤ 1.6μm for fatigue-critical areas.
Tight Production Schedule
The supplier needed 4 complete panel sets delivered within 8 weeks to meet the aircraft assembly milestone, leaving no room for rework or delivery delays.
Our Solution
Feiyin Self-Built Gantry 5-Axis Machining Center
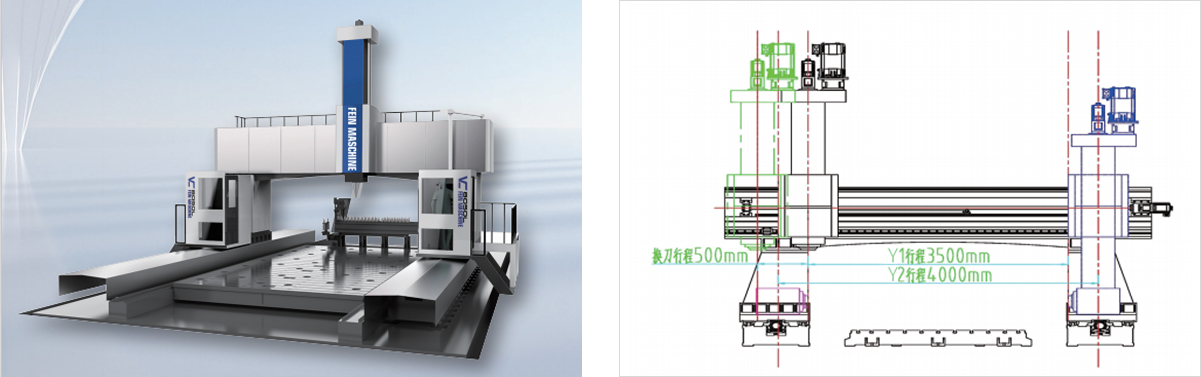
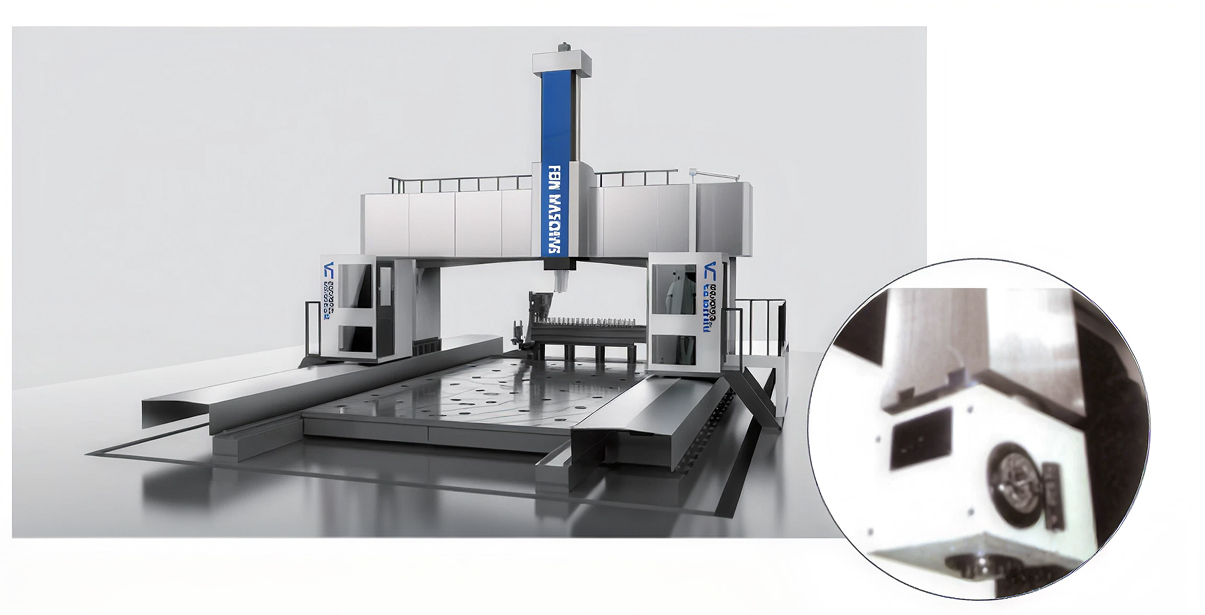
The project was machined on Feiyin's NQ-GV1060 gantry-type 5-axis machining center — a self-developed machine with a 10,600 x 2,600 x 1,200 mm work envelope. The gantry structure provides exceptional torsional rigidity across the full 9m span, critical for maintaining positional accuracy during extended traverses.
Custom Vacuum and Edge-Clamp Fixture System
A bespoke vacuum table combined with edge clamps was designed to secure the panel without distorting the 2.5mm thin webs. The fixture allowed the entire 9.2m panel to be loaded, machined, and inspected in a single station — eliminating re-clamping errors.
Dynamic Cutting Parameter Optimization
Feiyin's process engineering team ran FEA simulations of the cutting forces on the rib geometry before production. Cutting parameters were optimized to minimize deflection — using climb milling, controlled depth-of-cut per pass, and high-pressure cooling to manage heat input at the thin-web sections.
Feiyin Self-Built Gantry 5-Axis Machining Center
The project was machined on Feiyin's NQ-GV1060 gantry-type 5-axis machining center — a self-developed machine with a 10,600 x 2,600 x 1,200 mm work envelope. The gantry structure provides exceptional torsional rigidity across the full 9m span, critical for maintaining positional accuracy during extended traverses.
Siemens SINUMERIK 840D sl Control
The NQ-GV1060 is equipped with Siemens SINUMERIK 840D sl, enabling advanced real-time tool compensation and 5-axis simultaneous contouring with dynamic accuracy control across the full traverse range.
In-Process CMM Verification
Three CMM checkpoints were performed at key stages: after roughing, after semi-finishing, and before final finishing. ZEISS CMM was used with a reference temperature of 20°C to compensate for thermal expansion during machining.
 Full AS9102 Documentation Package
Every part was delivered with a complete first article inspection (FAI) report, CMM measurement data, material certificates, and Certificate of Conformance.
Project Results
First-Pass Yield Rate: 96%
Out of 4 complete panel sets (12 individual panels), only 1 minor rework was required on a single fastener hole location — successfully corrected in under 2 hours.
All 300+ Features Met ±0.015mm
Full CMM inspection confirmed every positional feature was within the ±0.015mm tolerance. No parts required scrap or re-machining due to out-of-tolerance conditions.
Delivered On Schedule
All 4 panel sets were shipped within the 8-week window, enabling the customer's wing assembly to proceed on the C919 production milestone schedule.
First-Time Repeat Order
The customer placed a repeat order within 3 months for two additional C919 wing panel sets — a direct result of the quality and delivery performance on the initial order.
Surface Finish: Ra 1.2μm Achieved
All fatigue-critical rib walls met Ra ≤ 1.6μm without post-machining hand finishing, verified by surface roughness tester at 10 measurement points per panel.

High Quality 5-Axis CNC Machine | Self-developed by Fein brand
Premium beam mobile 5-axis machines made with aerospace reliability. Competitive factory price, OEM/ODM accepted. Get free quote for your industrial workshop today.